Overview
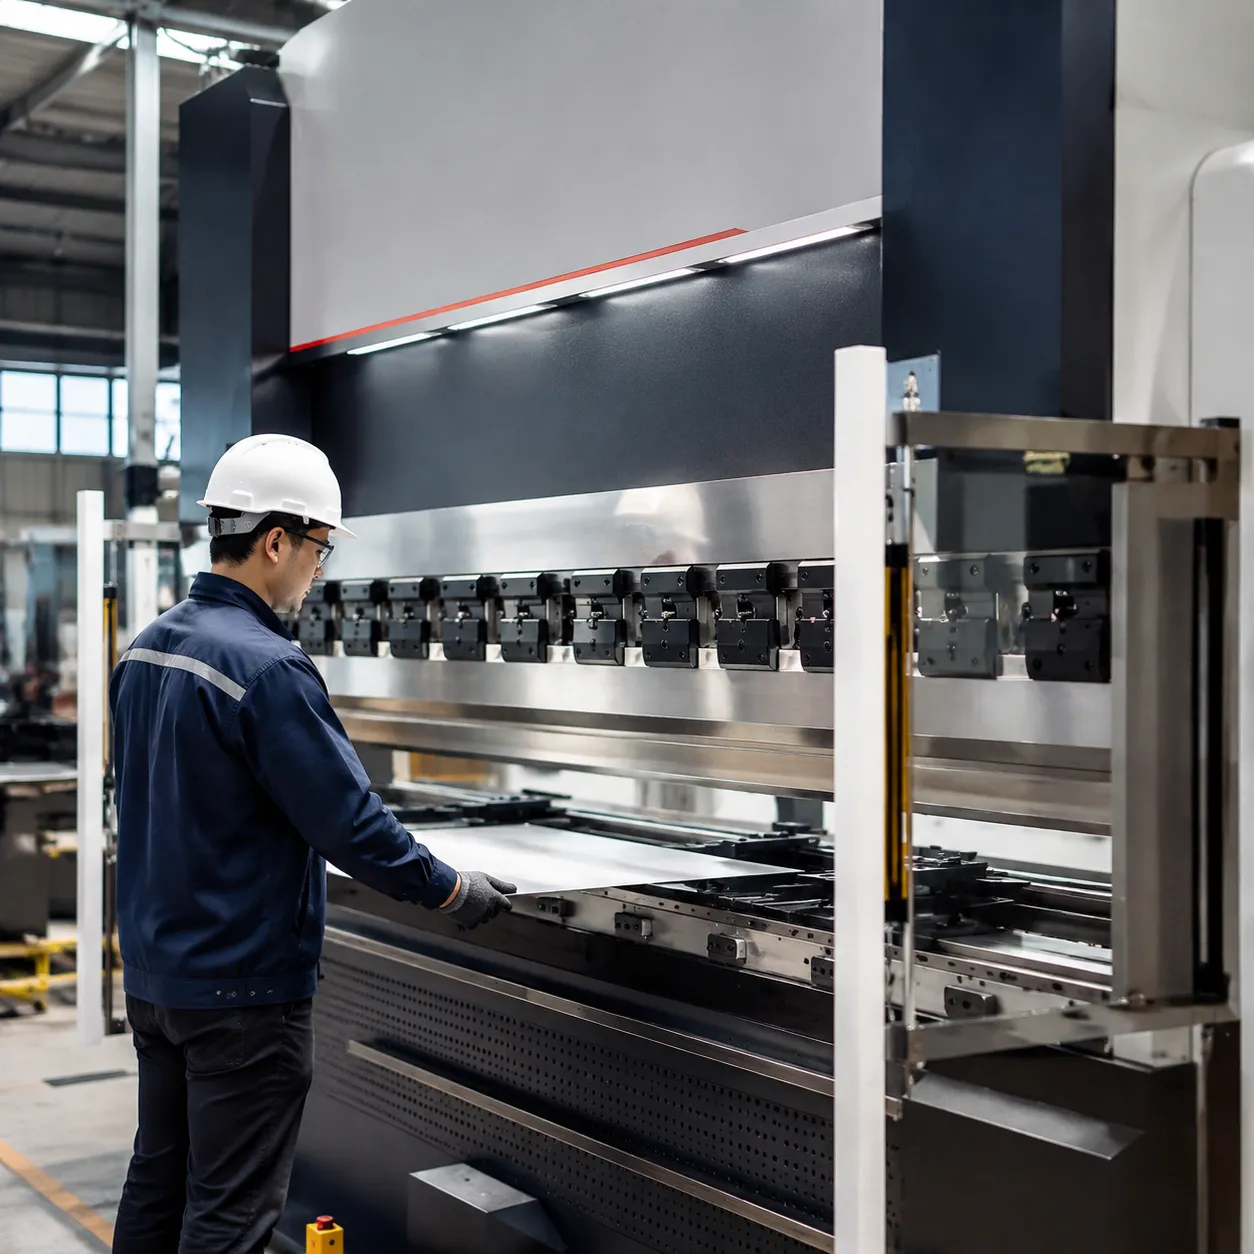
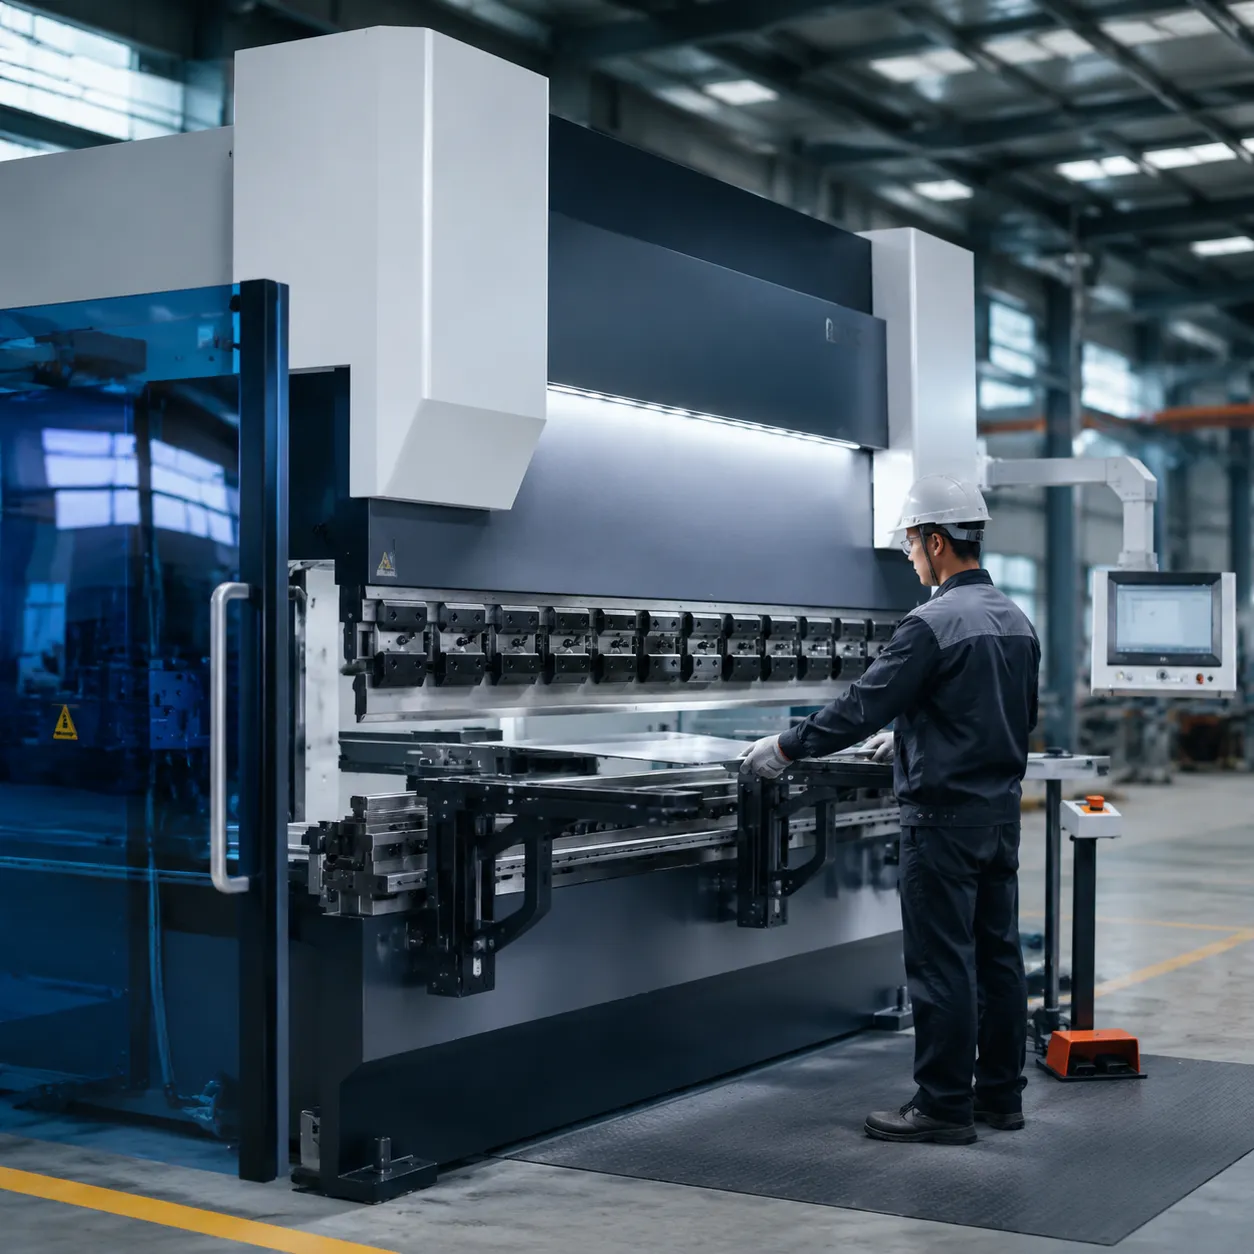
cnc bending machine da53t integrates a Delem touch screen press brake controller on hydraulic press brake frames with 4+1 axis control for precision sheet metal and carbon steel plate production.
Standard configurations span 40T–400T+ tonnage, bending length from compact shop beds to 4000 mm lines, and synchronized Y1/Y2 ram control with backgauge axis X R servo positioning.
Key Features of DA53T CNC Bending Machine
The Delem DA53T press brake controller on this hydraulic press brake eliminates operator guesswork, streamlines daily production, and delivers consistent precision across every bend in sheet metal fabrication cells.
| Axis | Control Function | Benefit |
|---|---|---|
| Y1 - Y2 | Synchronized hydraulic cylinders | Keeps the ram perfectly parallel, even under off-center loads. |
| X-axis | Horizontal backgauge movement | Delivers accurate flange length measurements automatically. |
| R-axis | Vertical backgauge height adjustment | Adapts seamlessly to varying die heights and Z-bends. |
Touchscreen Interface and 2D Graphical Programming
The touchscreen press brake controller simplifies complex part setup into a few taps on a durable 10.1-inch color screen. Operators sketch parts directly on the shop floor without needing advanced CAD skills.
- 2D graphical drawing: Draw the full sheet metal profile on-screen in seconds.
- Instant visual feedback: Real-time graphic view shows the exact workpiece shape during programming.
- Multi-touch control: Intuitive swipe-and-tap navigation reduces menu searching.
4-Axis Control Capabilities (Y1, Y2, X, R)
This 4 axis CNC press brake provides full control over ram positioning and backgauge movement, guaranteeing accurate bends on every cycle.
Automatic Bending Angle and Crowning Calculations
Achieving identical angles across full-length sheets requires precise control. The system calculates springback and bed deflection instantly.
- Bending angle calculation software: Input material type, thickness, and target angle; the system computes required press depth automatically.
- Automatic crowning control: Dynamically compensates for machine deflection on long carbon steel plates to deliver uniform angles from end to end.
Built-In Tool Library and Collision Detection
Tooling damage halts operations. Intelligent safeguard features protect dies and equipment on every hydraulic press brake cycle.
- Comprehensive tool library: Store specs for upper punches and lower dies for instant recall during setup.
- Real-time collision detection: Runs a safety simulation before bending to warn operators if the metal sheet will strike the backgauge or tooling.
How CNC Bending Machine DA53T Boosts Sheet Metal Efficiency
Test bends, manual gauge adjustments, and scrap plates cut into margins. Pairing a hydraulic bending machine frame with the Delem DA53T press brake controller removes those bottlenecks so operators spend more time forming parts.
Fast Part Setup on Complex Runs
Switching jobs shouldn't tie up a machine for half an hour. With 2D graphical programming and automatic bend calculations, setup time drops to minutes:
- Zero manual math: The system auto-calculates bend sequences, stroke depths, and tonnage limits.
- Instant tooling recall: Pull saved punch and die sets straight from the visual tooling library.
- Scrap-free first parts: Hit accurate angles right out of the gate on carbon steel plate, aluminum, and stainless sheet.
High Positioning Accuracy and Repeatability
Precision sheet metal bending demands tight tolerances from the first bend to the five-hundredth.
- Synchronized Y1-Y2 control: Dual hydraulic cylinder synchronization maintains ram leveling down to ±0.01 mm.
- Fast backgauge movement: High-speed servo motors position the backgauge axis X R with pinpoint accuracy, eliminating operator alignment error across multi-bend brackets.
Intuitive Touchscreen Navigation
New shifts do not require a dedicated programmer on every run. The touchscreen CNC bending controller runs on a crisp 10.1-inch color interface with clear graphical prompts that guide newer operators through part creation, tooling selection, and bending steps with zero guesswork.
| Shop Performance Factor | Standard Hydraulic Brake | CNC Bending Machine DA53T |
|---|---|---|
| Average Job Changeover | 15–25 minutes | Under 3 minutes |
| First-Piece Test Scrap | 2–4 test blanks per run | First-part good run |
| New Operator Ramp-Up | 2–3 weeks of training | Running production in 1–2 days |
| Idle Power Consumption | Continuous pump draw | On-demand power delivery |
Energy-Saving Servo-Hydraulic Integration
Pairing the DA53T with modern hybrid servo-hydraulic drives delivers hydraulic pressure strictly during active bending strokes. The system runs quietly, keeps oil temperatures lower during long production shifts, and cuts shop floor electric consumption by up to 40% compared to traditional constant-speed motor setups.
Core Specs and Axis Setups for CNC Bending Machine DA53T
| Spec Parameter | Compact Shop Setup | Standard Production | Heavy Fabrication |
|---|---|---|---|
| Bending Tonnage | 40 Tons - 80 Tons | 100 Tons - 160 Tons | 200 Tons - 400+ Tons |
| Bending Length | 4 ft - 8 ft | 10 ft - 13 ft | 13 ft - 20 ft+ |
| Control Axis Config | Y1, Y2, X, R (4-Axis) | Y1, Y2, X, R + V (4+1 Axis) | Y1, Y2, X, R, Z1, Z2 + V |
| Press Brake Controller | Delem DA53T Touch | Delem DA53T Touch | Delem DA53T / DA58T |
| Typical Material Range | 22 ga - 3/16 inch | 18 ga - 3/8 inch | 1/4 inch - 3/4 inch+ |
Y1-Y2 hydraulic cylinder synchronization
On a synchronized press brake with the Delem DA53T press brake controller, accuracy starts at the hydraulic cylinders. Y1 and Y2 operate independently using high-precision proportional valve technology and electronic linear encoders.
- Real-time monitoring: Both cylinders adjust constantly during the stroke to stay balanced within micro-meters.
- Off-center bending: Off-center loads stay balanced without twisting the ram or damaging the frame.
- Angle repeatability: Delivers identical bend angles across the entire length of carbon steel plate or stainless parts.
Backgauge axis movement (X and R axis setup)
A reliable 4 axis CNC press brake relies on a responsive backgauge to keep part throughput fast. The DA53T directly controls the backgauge axis X R positioning via servo drives.
- X-Axis (Depth): Servo-driven precision ball screws drive the backgauge fingers forward and backward for exact flange dimensions.
- R-Axis (Height): Motorized vertical movement automatically adjusts for multi-height dies and stepped bends.
- Positioning speed: High-speed drive loops eliminate waiting time between bend steps, driving up daily shop output.
Motorized CNC crowning system compatibility
Long metal sheet bending creates mechanical deflection in the bed and ram. Combining an automatic crowning CNC press brake with the DA53T eliminates center bowing effortlessly.
- V-Axis control: The DA53T calculates required crowning compensation based on tonnage, material thickness, and bending length.
- Motorized wedge system: Automatically adjusts the lower table profile before the punch hits the metal.
- No manual shimming: Gives you consistent, straight angles from end to end without wasting time packing tape or shims under the die.
Bending length and tonnage configurations
Programs configure hydraulic CNC bending machine models across several frame sizes for regional job shops and heavy production lines.
Delem DA53T CNC Programming and Tooling Library Workflow
Programming a CNC bending machine DA53T is fast, direct, and eliminates guesswork on the shop floor. The Delem DA53T press brake controller features a clear touchscreen interface that guides operators through setup in four simple steps, taking programs from raw sheet to accurate first-part bends without scrap using integrated CNC programming steps.
| Setup Step | Main Action | System Calculation |
|---|---|---|
| 1. Material Setup | Input sheet thickness, length, and material type | Target tonnage and springback allowance |
| 2. 2D Profile | Sketch part geometry and angles on screen | Digital part profile and flange dimensions |
| 3. Tooling | Select punch and die from tooling library | Tool clearance zones and load limits |
| 4. Auto Sequence | Run automatic sequence optimizer | X/R backgauge positions and collision check |
Workpiece Material and Sheet Thickness Setup
Every program starts on the setup screen to define basic part parameters:
- Select Material: Pick carbon steel, stainless steel, or aluminum from the pre-loaded library.
- Set Sheet Dimensions: Input exact sheet thickness and overall bending length.
- Verify Tensile Strength: Ensure yield strength values match your material lot so the system accurately computes force requirements.
2D Graphical Profile Drawing
The 2D graphical press brake control on the Delem touch screen supports direct part drawing on the panel:
- Tap the screen to sketch part segments step-by-step.
- Enter required flange lengths and target metal bending angle values.
- Use finger gestures to adjust dimensions or insert radius bends instantly.
Punch and Die Tooling Selection
Assigning the right press brake punch and die tooling protects tooling and guarantees part accuracy:
- Access the graphical tooling library directly from the screen.
- Select your upper punch geometry and radius.
- Select the correct lower die V-groove opening for your sheet thickness.
- Confirm tool placement positions on the beam.
Auto Bend Sequence and Backgauge Calculation
Once part profile and tools are set, the integrated bending angle calculation software handles the heavy lifting:
- Bend Sequencing: The system automatically calculates the most efficient, collision-free bend order.
- Positioning: Automatically computes required positions for the backgauge axis X R movement for every step.
- Pressure & Crowning: Calculates optimal hydraulic tonnage and automatic crowning settings before the ram drops.
CNC Bending Machine DA53T Maintenance and Hydraulic Press Brake Care
Peak performance on a cnc bending machine da53t depends on consistent daily habits and proper controller maintenance across hydraulic press brake shifts.
Daily Inspection and Hydraulic Oil Temperature Checks
Hydraulic performance directly impacts bend accuracy. Inspect these items before the first shift:
- Fluid Levels & Leaks: Inspect the sight glass on the hydraulic reservoir and check cylinder seals for oil seepage.
- Oil Temperature Monitoring: Keep hydraulic oil operating between 100°F and 130°F. High heat degrades fluid viscosity, causing tonnage drift during long production runs.
- Filter Condition: Watch the clog indicator on the return line filter to prevent pump cavitation.
Calibration Procedures for X and R Backgauge Axes
To maintain precise flange lengths, the backgauge axis X R requires periodic zero-point calibration.
- Execute Homing: Run the automatic reference search on the Delem DA53T press brake controller during startup.
- Physical Verification: Program a simple 90-degree bend, measure the actual flange dimension with digital calipers, and compare it to the target position.
- Offset Adjustment: If you spot a variance, open the axis parameter page on the Delem touch screen and adjust the axis offset value directly to bring backgauge depth and finger height back into spec.
Software Updates and USB Data Backup Steps
Protect custom tooling library profiles and bend sequences with a strict backup routine using the front USB port on the Delem panel.
- Format Drive: Use a standard USB drive formatted to FAT32.
- Export Tooling & Programs: Navigate to the main menu, select Backup/Restore, and save all tooling libraries, machine parameters, and product files.
- Routine Software Patches: Keep the Delem control software updated to access improved angle calculation algorithms and patch stability bugs.
Troubleshooting Common DA53T Controller Alarm Codes
When an alert interrupts production, the built-in Delem controller troubleshooting guide helps operators diagnose and clear alarms quickly.
| Alarm / Message | Likely Cause | Quick Solution |
|---|---|---|
| Y1/Y2 Synchronization Error | Proportional valve dirt or scale feedback fault | Check linear encoder cleanliness; clean hydraulic valves. |
| X-Axis Positioning Fault | Backgauge mechanical obstruction or motor drive trip | Inspect ball screw for debris; check servo drive status. |
| Emergency Stop Active | E-stop button depressed or safety light curtain tripped | Reset physical E-stop buttons; check optical barrier alignment. |
| Pressure Limit Reached | Target bend requires tonnage exceeding machine limit | Verify material thickness and sheet strength settings on controller. |
Share tonnage, bending length, material gauge, and controller options for itemized cnc bending machine da53t pricing—Contact ProMach with DXF bend profiles and voltage specification.
Industrial Applications for CNC Bending Machine DA53T
cnc bending machine da53t cells serve high-mix sheet metal fabrication
lines where metal sheet bending, flange accuracy, and quick changeovers matter. Pair baseline
hydraulic bending machine duty with
CNC bending machine for sheet
metal layouts when comparing standalone versus automated cells.
Precision Enclosures and Electrical Fabrication
- Control cabinets and switchgear: Multi-bend panels with tight metal bending angle control on galvanized and stainless sheet.
- Busbar and copper work: Short-run prototypes through repeat production with 4+1 axis control backgauge positioning.
- Server and telecom racks: Long flange runs on carbon steel plate and aluminum with crowning compensation.
HVAC, Architectural, and Heavy Fabrication
- Duct and filtration: High-volume precision sheet metal segments with collision-checked tooling library profiles.
- Facade and signage: Variable-radius bends on mixed gauges without manual shim packing.
- Heavy plate structures: 200T–400T+ hydraulic press brake frames for thick carbon steel plate brackets and structural stiffeners.
For segmented punch and die changeovers, see
CNC bending machine tools paired with
the DA53T press brake controller for quick-setup production.
OEM Configuration and Ordering
OEM builds configure frame tonnage, bending length, voltage, safety packages, and controller
firmware to match plant standards. Standard lead times typically run 30–45 days from approved drawings; MOQ starts
at 1 set for catalog frames with custom tooling quoted separately.
- Controller options: Delem DA53T standard; DA58T or DA66T upgrades for larger visualization when specified.
- Axis packages: Y1/Y2/X/R base; optional V crowning and additional Z fingers on heavy synchronized press brake lines.
- Factory support: Remote diagnostics, parameter backup templates, and operator training scope included in OEM quotes.
- Documentation: Electrical schematics, hydraulic layouts, and CNC programming quick-start guides supplied before shipment.
Controller workflow fundamentals align with
how a CNC bending machine works across
mixed sheet metal fabrication cells.
Frequently Asked Questions About CNC Bending Machine DA53T
Direct answers on DA53T versus DA58T, offline CNC programming, axis counts, and job-shop versus heavy hydraulic press brake duty.
| Question | Answer |
|---|---|
| Delem DA53T vs. DA58T: What is the difference? | Shop owners often compare controller tiers when specifying a new line. Both units deliver excellent precision for sheet metal fabrication, but they cater to different screen sizes and visual preferences.
|
| Can the DA53T handle offline programming software? | Yes. Delem Profile-T 2D offline software keeps machines bending while CNC programming runs on a PC, then loads files to the Delem touch screen via USB.
|
| What Is the Difference Between Press Brake Controller and Offline CNC Programming? | The onboard press brake controller handles live setup, tooling library recall, and metal bending angle calculations at the machine. Offline CNC programming on a PC drafts profiles first, then transfers them to the Delem touch screen without stopping production. |
| How many axes can a DA53T press brake control simultaneously? | A typical CNC bending machine DA53T manages a 4+1 axis control setup:
|
| Is the DA53T suitable for small job shops and heavy fabrication? | Yes. Catalog frames handle quick job-shop changeovers through heavy carbon steel plate production on the same press brake controller backbone.
Send material thickness, tonnage, and tooling library requirements via Contact ProMach for controller pairing review. |